

Overview
Read this article from a comprehensive knowledge base, updated and supplemented with articles reviewed by scientific committees.
Read the articleAUTHORS
-
Guy BOSTBARGE : Arts et Métiers engineer - General Manager, Société Amis
-
Henri FAURE : Engineer from Arts et Métiers and École Supérieure de Soudure Autogène - Director of Société Amis
-
Yann GOBARD : Engineer from the École Supérieure de l'Énergie et des Matériaux and graduate of the Centre de Mise en Forme de l'École des Mines de Paris Deputy Production Manager and Head of the Engineering and Methods Department at Amis.
INTRODUCTION
Hot forging (free forging or die forging) is well known to everyone. Some people might think that cold forging of steel consists in carrying out similar work, without prior heating. But the forces required would be such that similar tools would not withstand them, and cold forging of steel (forging in a tool with a parting line) ultimately has few industrial applications.
Cold forging, or extrusion, consists of producing parts by using tools to force the metal to flow in one or more directions. Pressures on tools can exceed 2 GPa, and lateral forces resulting from significant dissymmetry would condemn tools of insufficient strength, which is the main limit to their use.
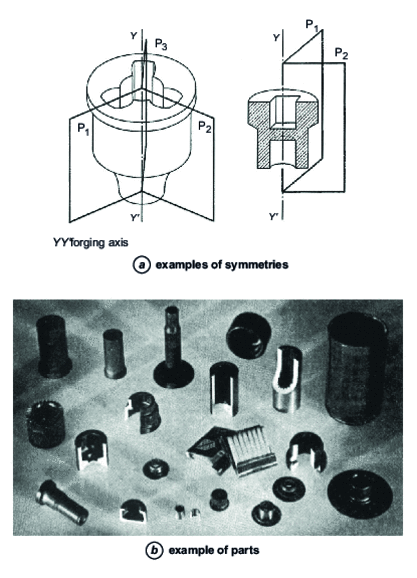
With a few rare exceptions, the parts in question feature at least two planes of symmetry, the intersection of which constitutes the forging axis. Various polygonal shapes and cylindrical shapes of revolution can be combined on the same part, provided they retain either the same axis, or a symmetry in the distribution of their axes (figure 1).
The second limit is the deformability of the metal used. The ductility of steel varies greatly with temperature (figure 2).
For certain limit applications (grades with a high carbon content ––, high deformation rates due to complex geometries, etc.), it may be necessary to heat to an intermediate temperature, 550 to 800°C: this is known as mid-hot forging.

Exclusive to subscribers. 97% yet to be discovered!
Already subscribed? Log in!
Steel cold forging - Steel selection and processes
 Process description
Article included in this offer
"Metal forming and foundry"
(
126 articles
)
Updated and enriched with articles validated by our scientific committees
A set of exclusive tools to complement the resources
